
What Causes Welding Spatter and the Five Adjustments That Reduce It
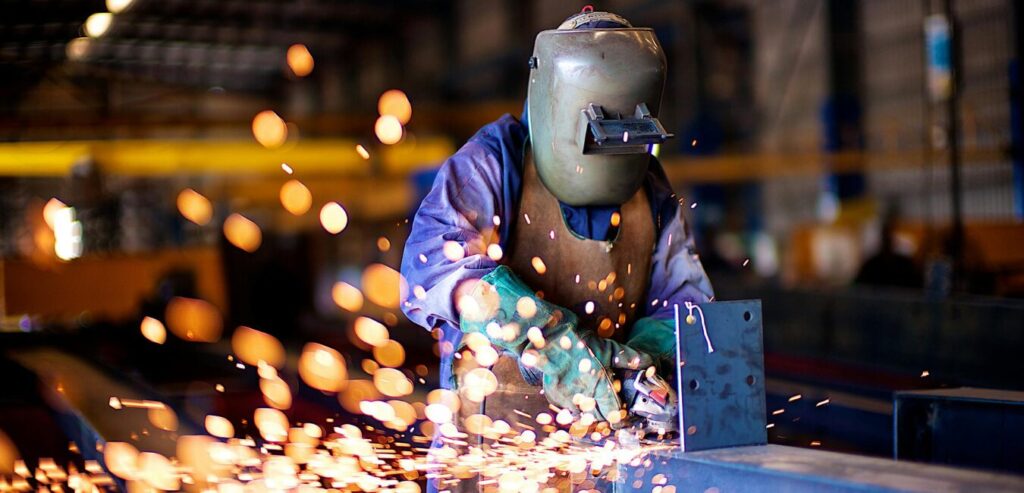
Some spatter is normal in MIG and flux core welding. Small droplets of molten metal fly off the arc and land on the workpiece, the table, and you. But when spatter goes from a light dusting to a constant shower of hot metal, something is wrong with your setup. Understanding what causes welding spatter is the first step toward fixing it, and in most cases the fix is a settings adjustment, not a new machine.
This post covers the five most common causes and the matching adjustments that serve as a MIG welding spatter fix for each one.
What Causes Welding Spatter
Spatter happens when molten metal is expelled from the weld pool or the wire tip instead of being deposited into the joint. Several conditions cause this, and most trace back to instability in the arc. Here is what causes welding spatter in the majority of cases:
| Cause | Why It Creates Spatter |
|---|---|
| Voltage too low or too high | Arc becomes unstable, metal transfers erratically |
| Wire feed speed mismatch | Too fast causes stubbing; too slow causes globular transfer |
| Wrong or insufficient shielding gas | Atmosphere contaminates the arc, disrupting transfer |
| Dirty base metal | Paint, oil, rust, and mill scale react in the arc |
| Wrong polarity | Incorrect current direction destabilizes the process |
| Worn contact tip | Poor electrical contact causes arc wander |
| Excessive stickout | Wire overheats before reaching the arc |
When you have welding spatter too much for what the job should produce, work through this list systematically. Usually one or two of these causes are the culprit.
Fix 1: Dial In Your Voltage
Voltage controls the arc length and the way molten metal transfers from the wire to the puddle. Too low and the wire stubs into the work, creating a harsh, popping arc that throws metal. Too high and the arc becomes wide and wandering, which also ejects spatter.
The MIG welding spatter fix for voltage is to start at the manufacturer’s recommended setting for your wire diameter and material thickness, then fine-tune by ear and eye. A smooth, crackling arc with consistent fry sound is the target. If it pops and crackles unevenly, adjust voltage in 0.5V increments until the sound stabilizes.
Fix 2: Match Your Wire Feed Speed
Wire feed speed and voltage work together. Too fast and the wire stubs into the workpiece, creating too much welding spatter for a clean bead. Too slow and the wire melts in large droplets (globular transfer) that fall irregularly.
The goal is short-circuit transfer: the wire touches the puddle, creates a short circuit, and current pinches off a small droplet. This cycle repeats 60 to 200 times per second, producing the smooth frying-bacon sound. Adjust wire feed speed in small increments while keeping voltage stable.
Fix 3: Check Your Shielding Gas
100% CO2 is cheap but produces more spatter because it creates a more aggressive arc. A 75% argon / 25% CO2 blend (C25) is the standard for mild steel MIG because it balances penetration with a smoother arc.
If you are wondering how to reduce welding spatter, switching to a 75/25 argon/CO2 mix is often the single most effective change. Check your flow rate with a regulator too. Under 15 CFH leaves the arc unshielded. Over 30 CFH creates turbulence. The sweet spot is 20 to 25 CFH for most indoor MIG work.
Fix 4: Clean the Metal and Check the Contact Tip
Dirty base metal is a guaranteed source of welding spatter too much to tolerate. Paint, oil, rust, mill scale, and coatings all react when heated by the arc, disrupting the gas shield and destabilizing metal transfer.
If you want to know how to eliminate spatter when welding on questionable surfaces: grind, wire brush, or wipe with acetone before striking an arc. This is the lowest-cost, highest-impact MIG welding spatter fix available.
While you are at it, check the contact tip on your MIG gun. A worn, enlarged, or spatter-clogged contact tip causes poor electrical contact with the wire. That creates arc wander and erratic transfer. Contact tips are consumables. Replace them regularly. If you are running through a spool of wire without swapping the tip, it is overdue.
Fix 5: Correct Your Technique
Even with perfect settings, bad technique causes spatter:
- Excessive stickout: keep it between 3/8 inch and 5/8 inch. Longer stickout overheats the wire before the arc and produces erratic transfer.
- Pushing instead of dragging with flux core. Flux core should be dragged. Pushing traps slag and increases spatter.
- Travel speed too fast. The puddle cannot absorb filler metal fast enough, and droplets ricochet.
- Wrong work angle. Keep the gun at 10 to 15 degrees in the travel direction and 45 degrees on fillet welds.
Knowing how to eliminate spatter when welding is partly settings and partly technique. If your settings are dialed and spatter persists, how you hold and move the gun is the remaining variable.
When Spatter Is Normal
Zero spatter is not realistic for MIG or flux core. Even with perfect settings, some will land on the workpiece. Anti-spatter spray on the nozzle and work surface helps cleanup. The question of how to reduce welding spatter is about getting it to an acceptable level. If your beads are clean, penetration is solid, and spatter wipes off with a brush, you are in the right range.
Getting the Right Consumables at CryoWeld
Most spatter problems trace back to settings, gas, or consumables. CryoWeld carries welding wire, shielding gas, contact tips, nozzles, MIG torches, and welding machines from Lincoln Electric at both Hudson Valley locations.
Call Poughkeepsie at (845) 473-3357 or Lake Katrine at (845) 336-8680, weekdays 8 to 5. Or visit cryoweld.com.
FAQs
Why is my MIG welder producing so much spatter?
The most common causes are incorrect voltage (too high or too low), wire feed speed that does not match the voltage, wrong shielding gas mix, dirty base metal, or a worn contact tip. Work through each variable systematically. Most MIG welding spatter fix adjustments are small, incremental changes to voltage and wire speed.
Does too much voltage cause welding spatter?
Yes. Excessive voltage creates a wide, unstable arc that ejects molten droplets. Too little voltage also causes spatter by creating a harsh, stubbing arc. The correct voltage produces a smooth, crackling sound with consistent metal transfer. Adjust in 0.5V increments.
What shielding gas reduces MIG welding spatter?
A 75% argon / 25% CO2 blend (C25) produces significantly less spatter than 100% CO2. The argon component smooths the arc and promotes a more stable short-circuit transfer. For stainless steel, a tri-mix with helium further improves arc stability and reduces spatter.
Does welding wire type affect spatter?
Yes, copper welding wire like ER70S-6 feeds more smoothly and arcs more consistently than uncoated wire. Wire that is contaminated, rusty, or stored in damp conditions causes erratic feeding and increased spatter. Always store wire sealed and dry.
How do you stop flux core welding from spattering so much?
Flux core inherently produces more spatter than solid MIG wire. Use the correct polarity (DCEN for self-shielded, DCEP for gas-shielded), drag the gun instead of pushing, keep stickout short, and make sure voltage and wire speed are matched to the wire manufacturer’s recommendations. Anti-spatter spray on the nozzle and work surface helps with cleanup.